
High-Frequency Vibration Feather Orientation Feeder
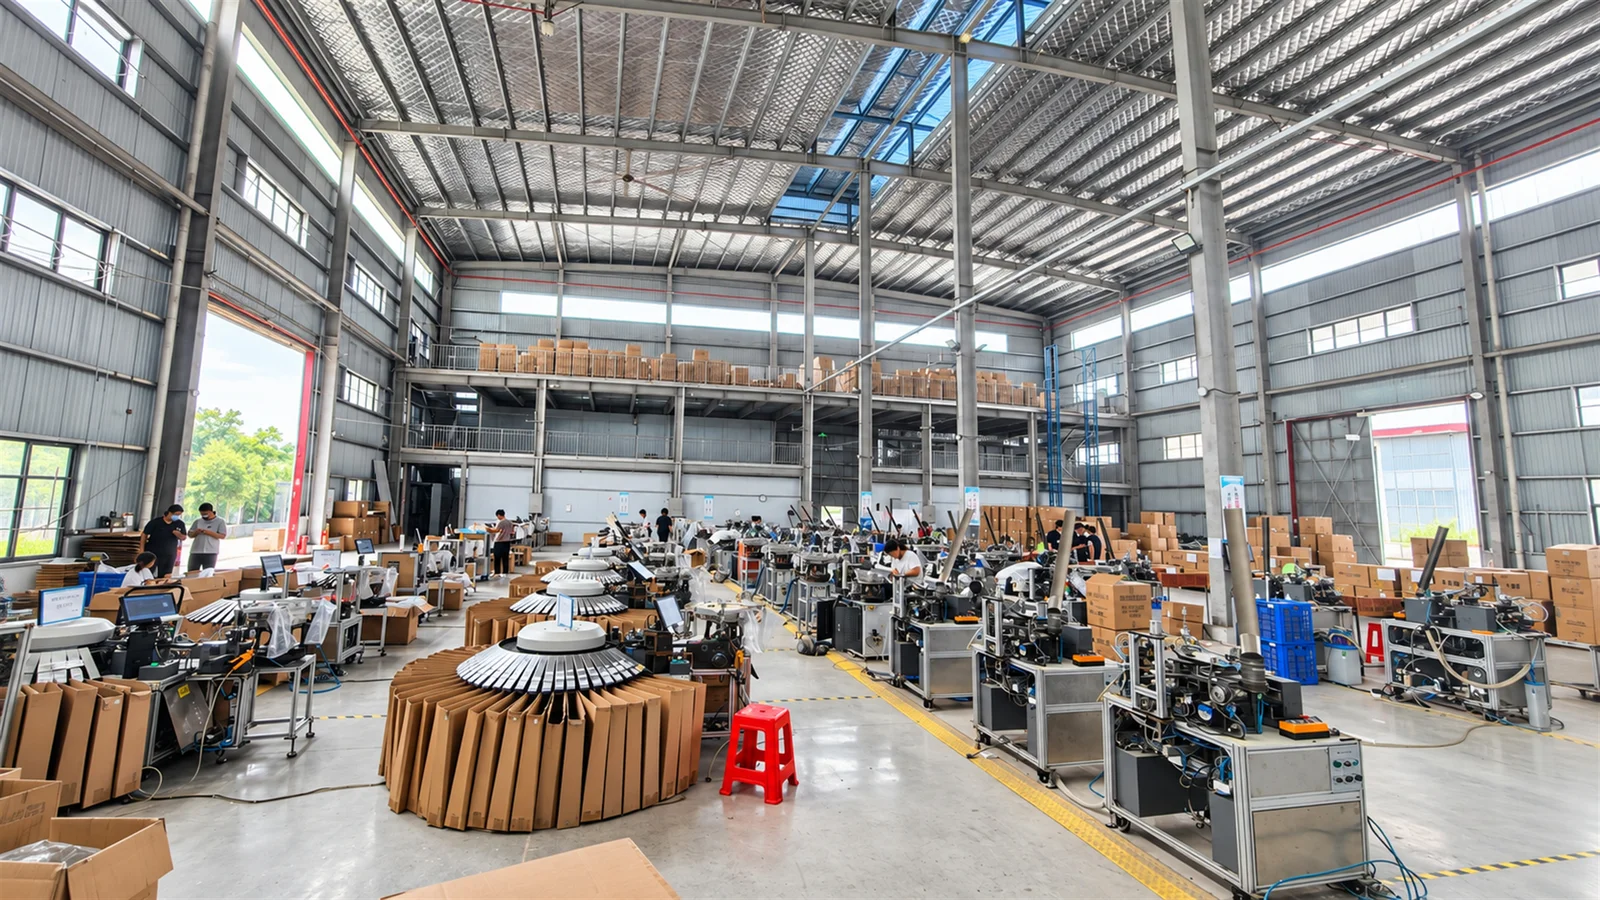
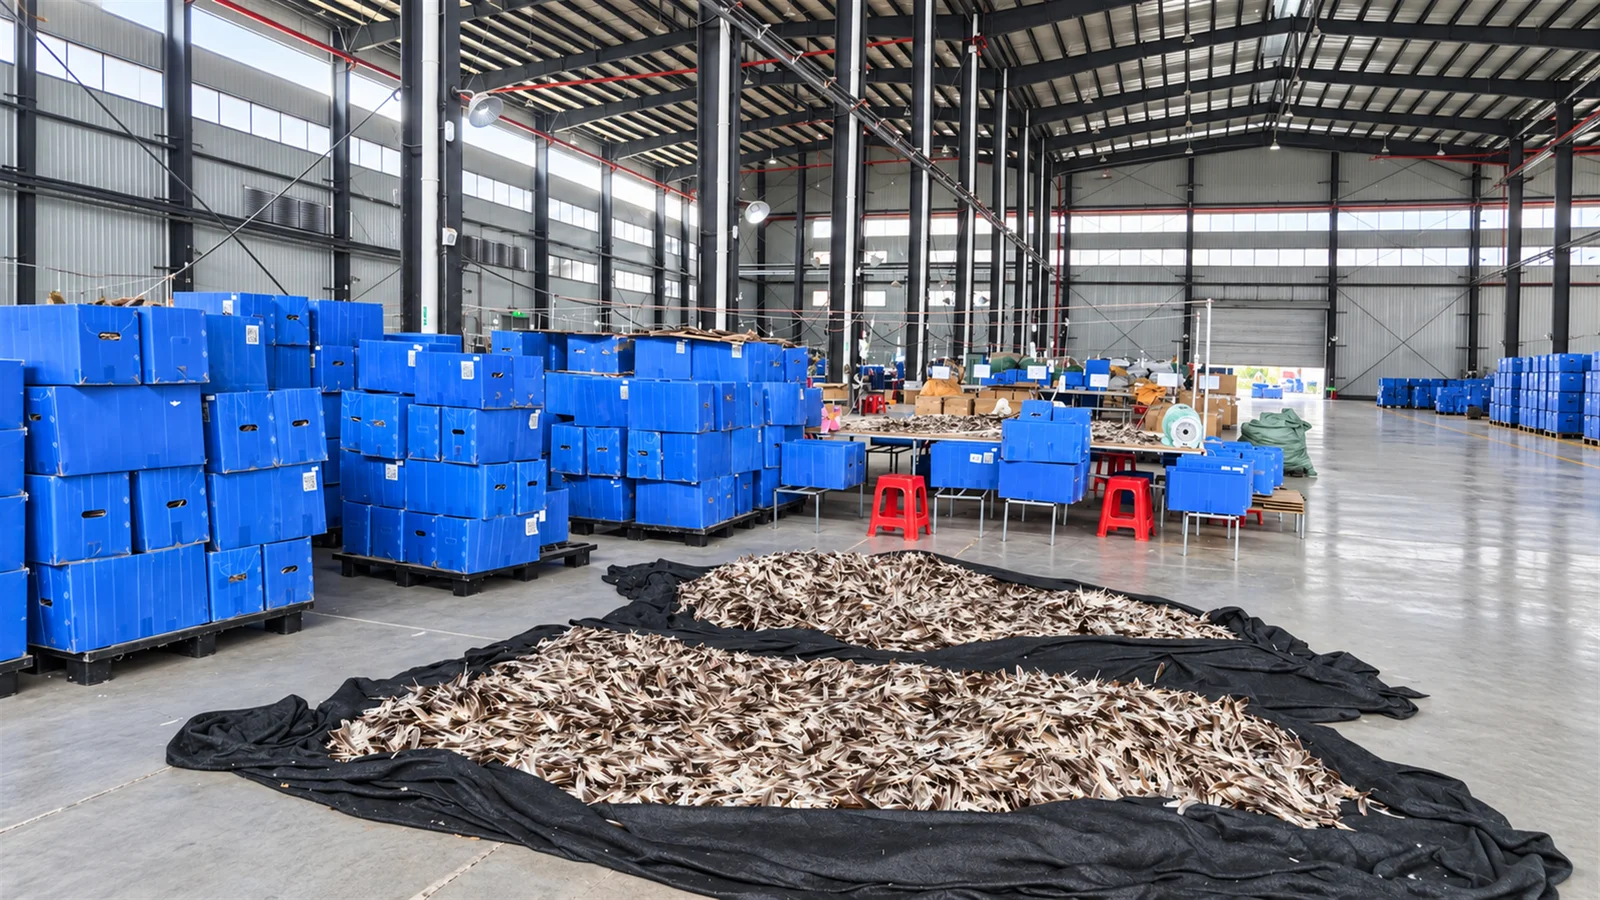
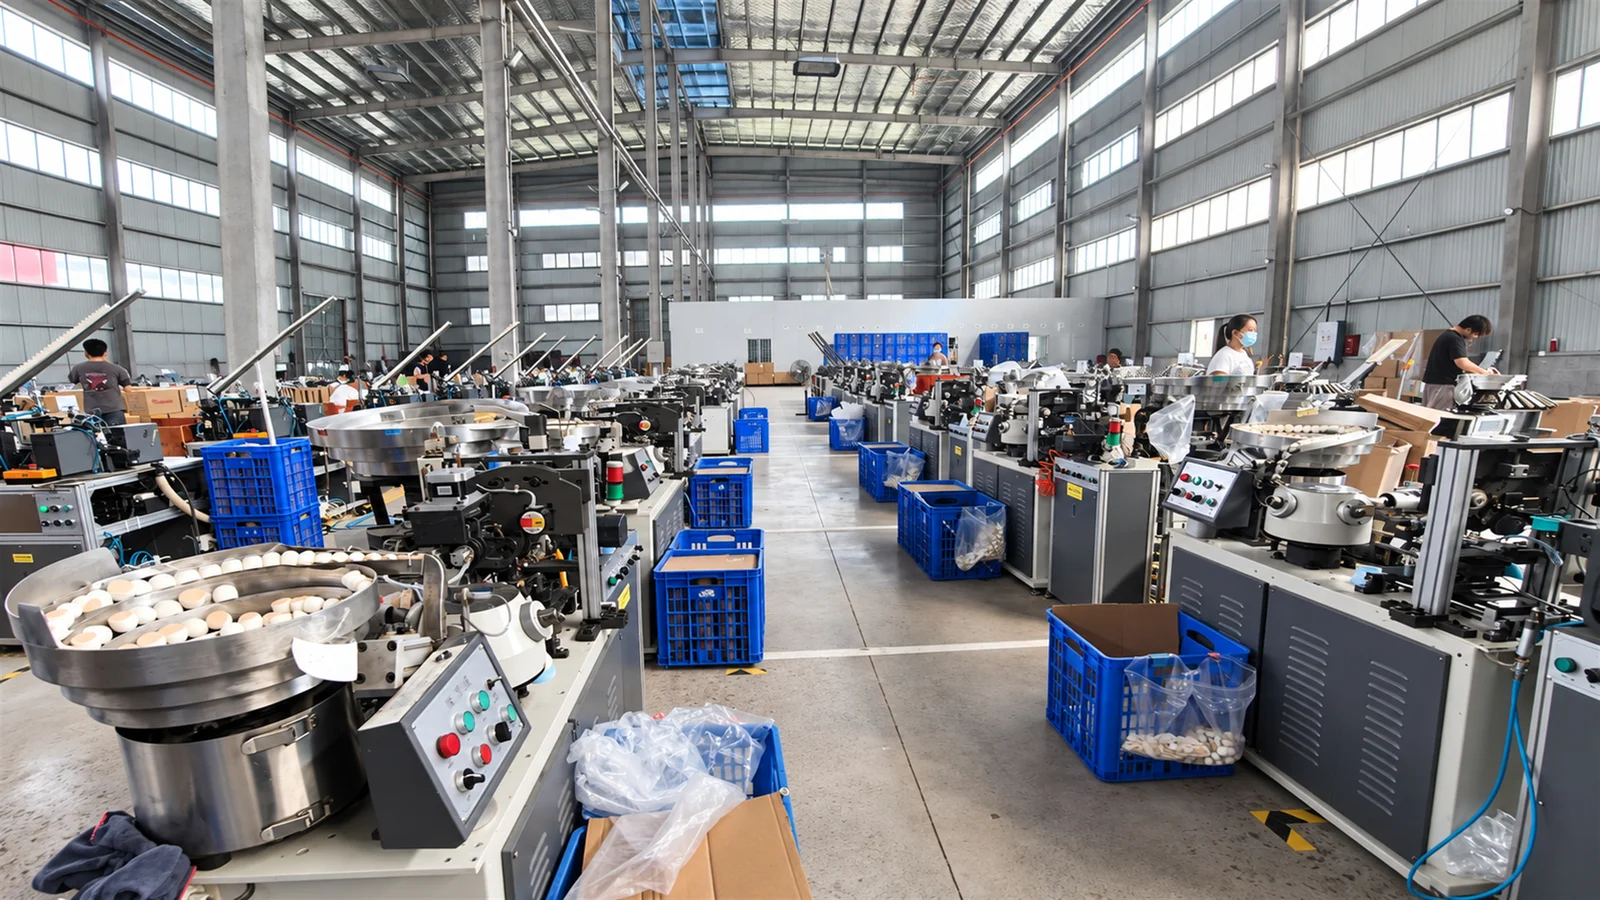
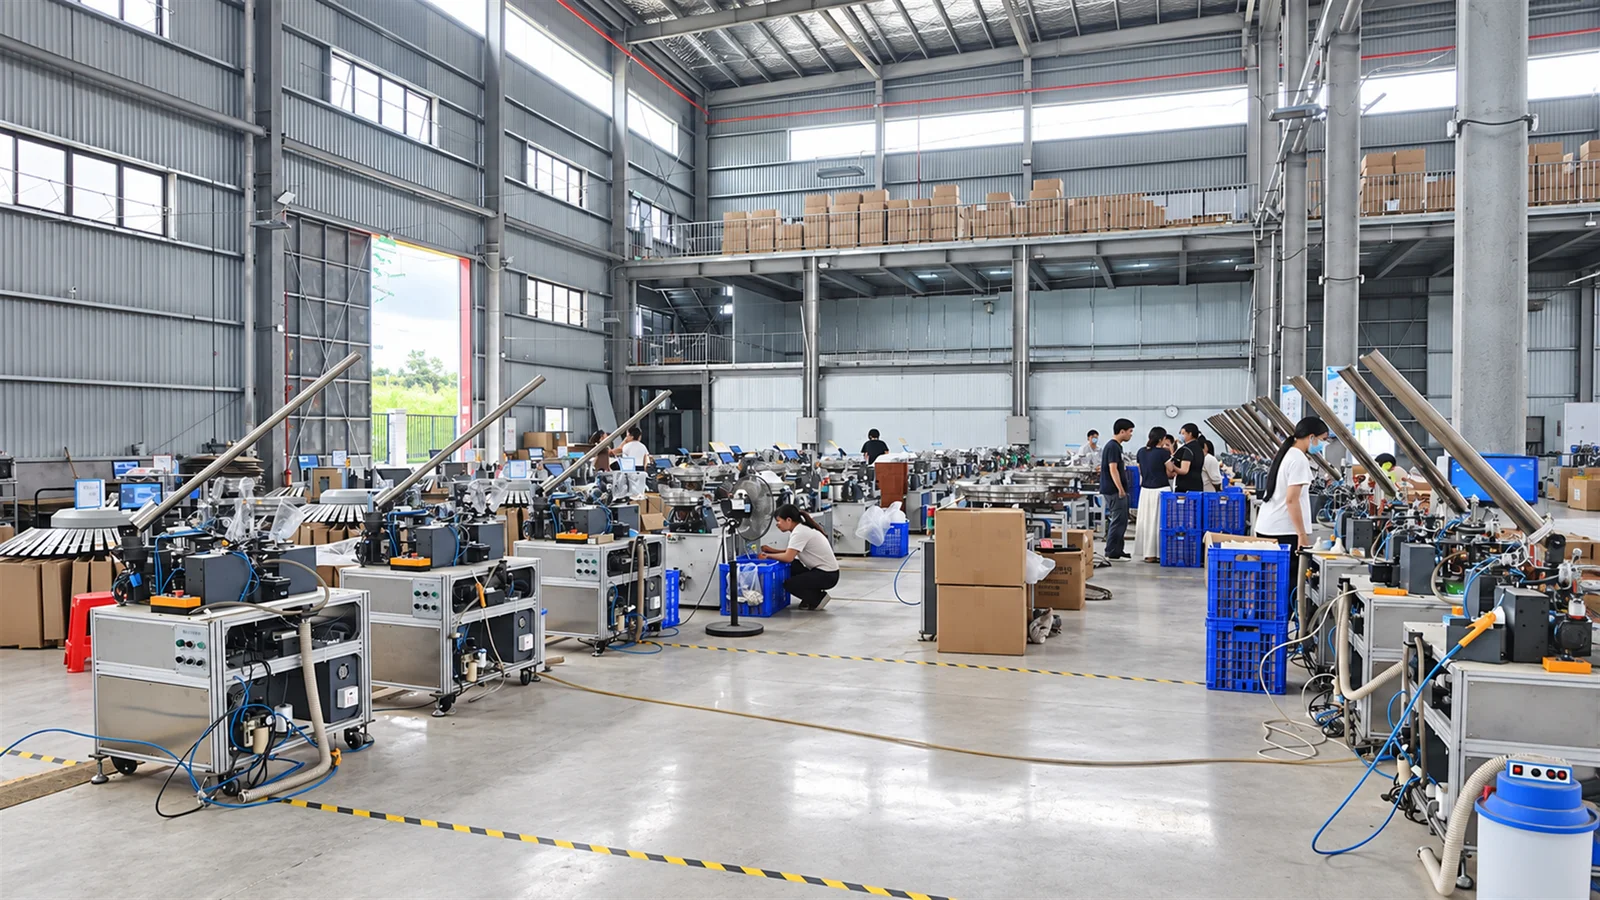
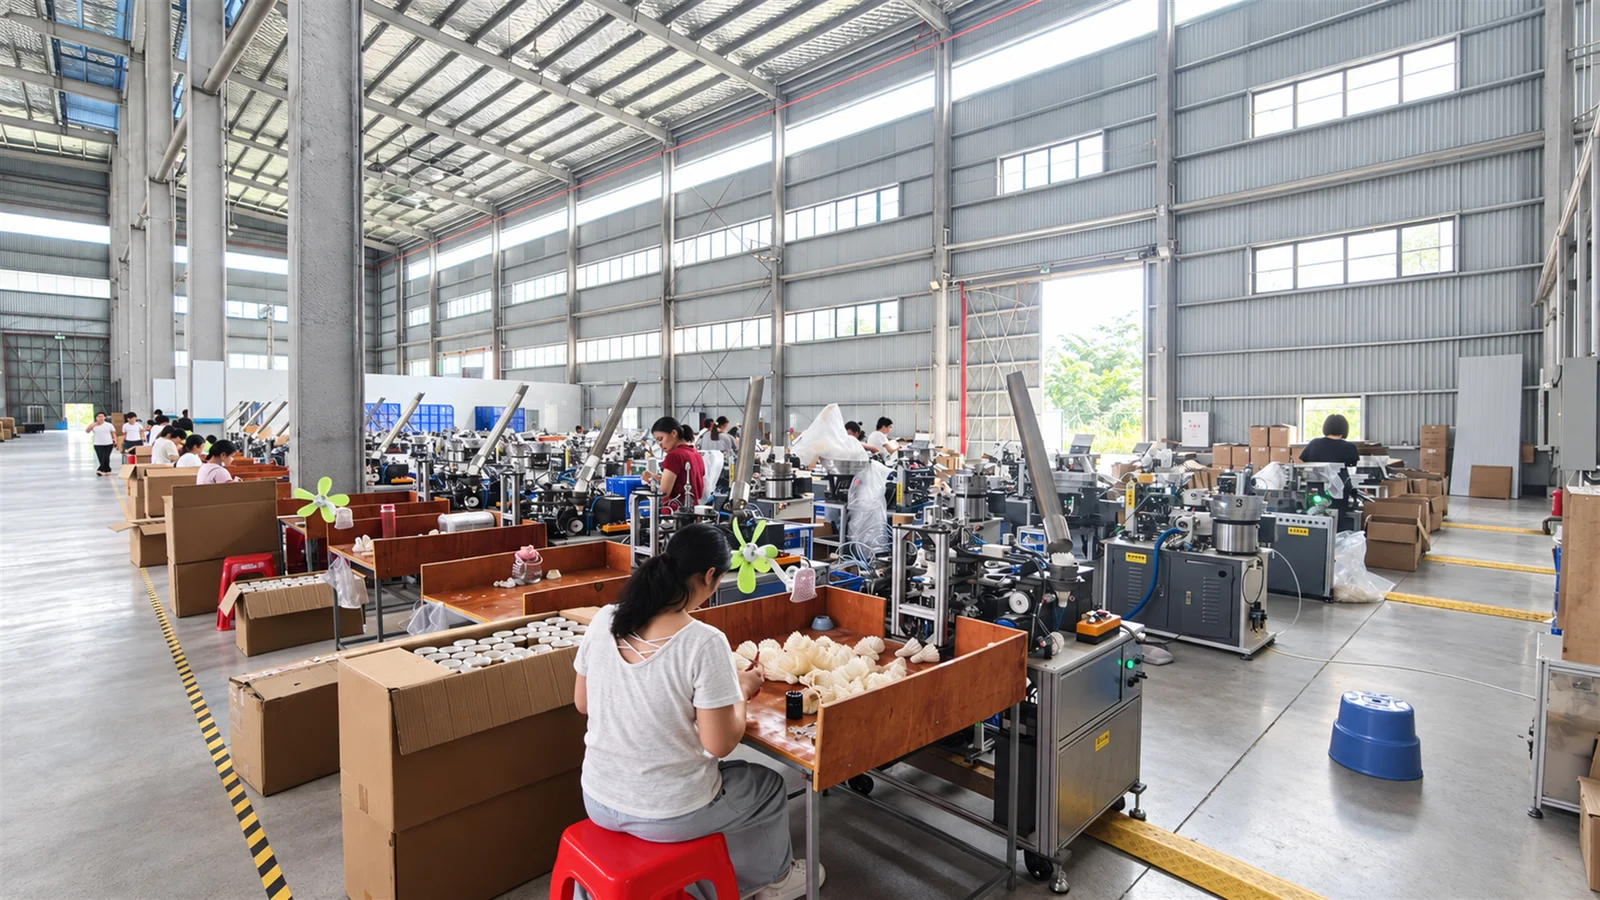
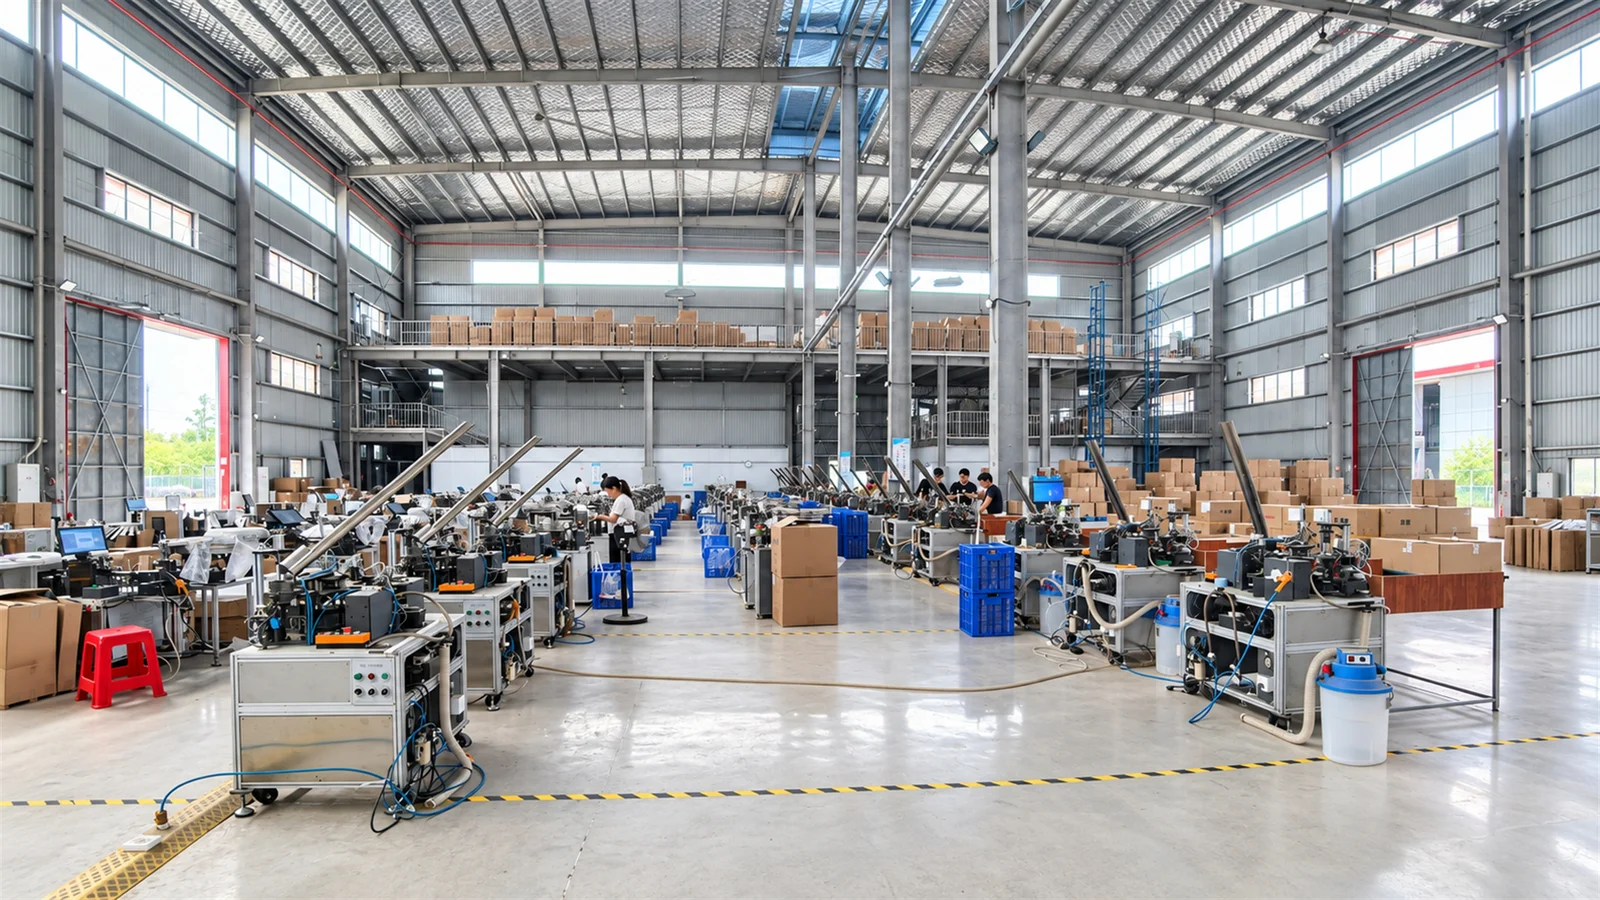
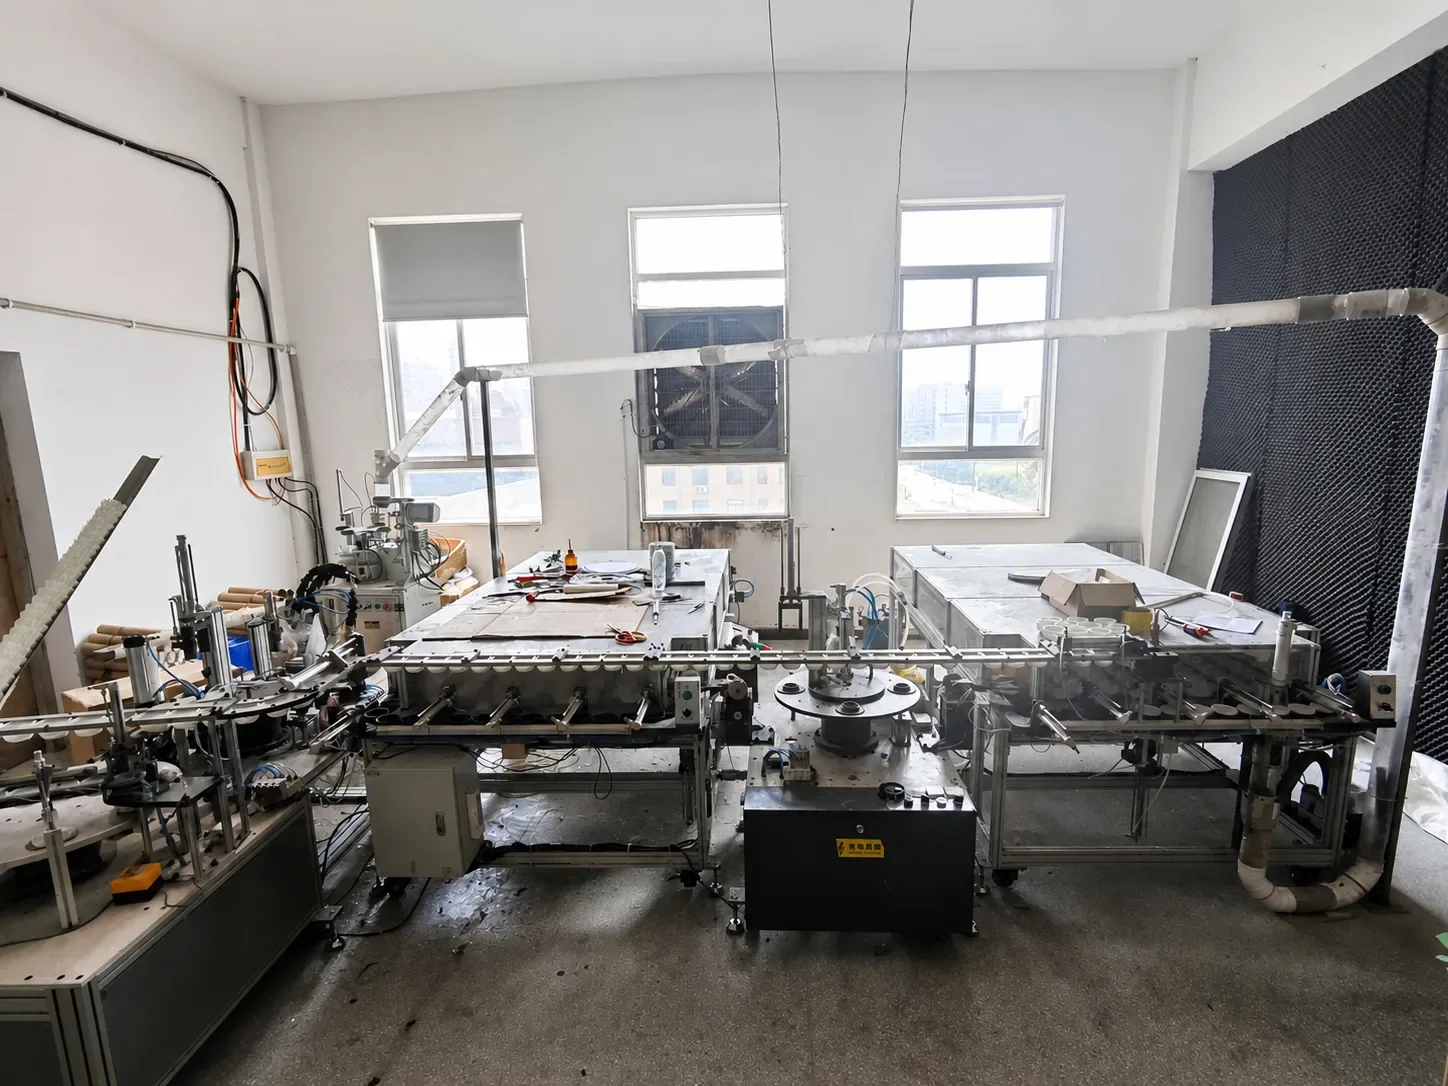
Microcomputer-controlled tuned vibration arranges bulk raw feathers in an orderly single-file flow, feeding undamaged quills smoothly into the optical inspection channels.

We provide global buyers with one-stop custom OEM services for tournament feather shuttlecocks featuring both superior price and quality competitiveness.
Microcomputer-controlled tuned vibration arranges bulk raw feathers in an orderly single-file flow, feeding undamaged quills smoothly into the optical inspection channels.

High-resolution industrial vision cameras scan quill curvature (±0.1°), arch, and dimensions in milliseconds, triggering pneumatic valves for multi-tier micro-sorting.

Classified Grade-A goose and premium duck feathers guide through parallel precision channels, ensuring over 99% geometric symmetry across all 16 vanes of each shuttle.

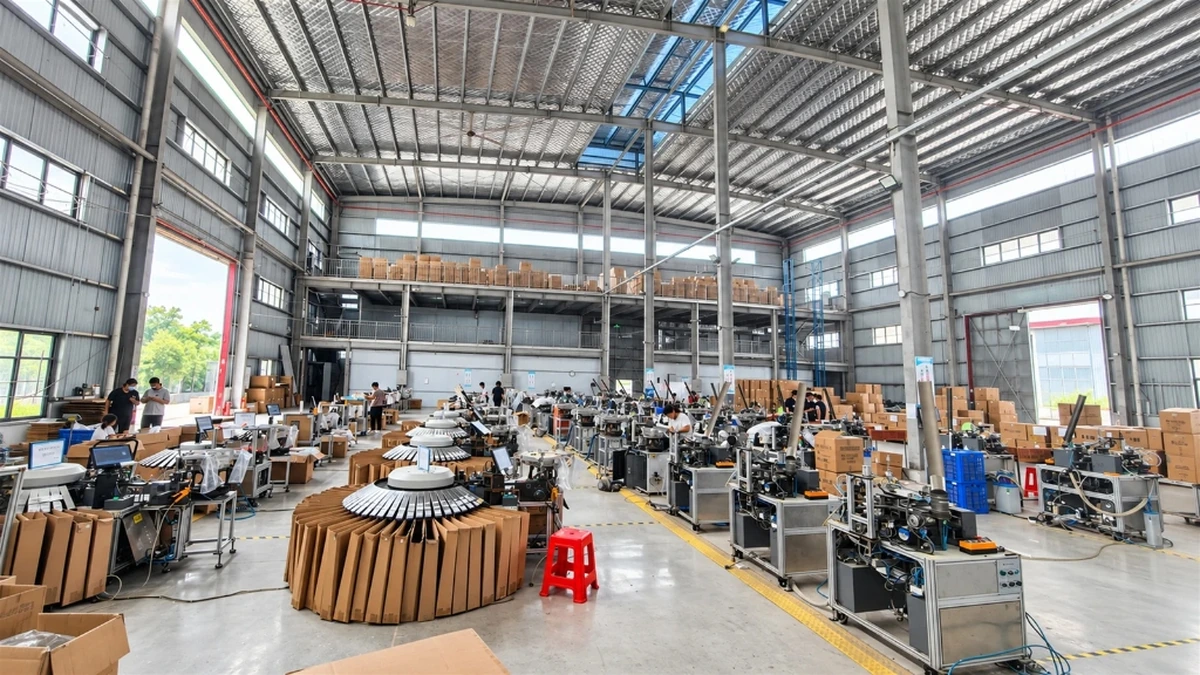
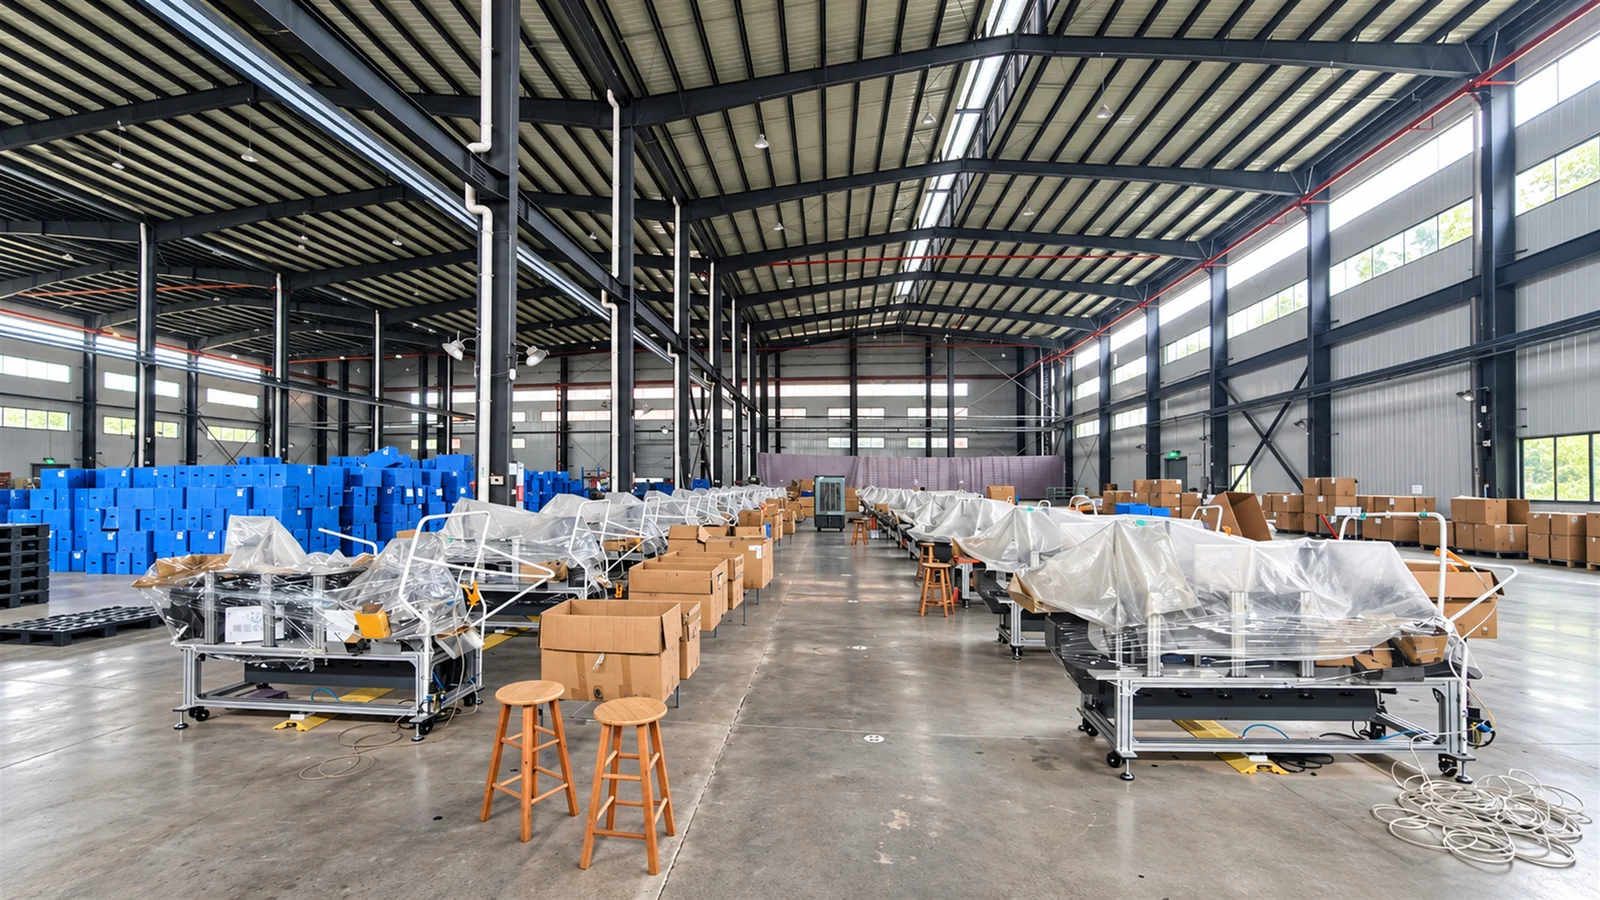
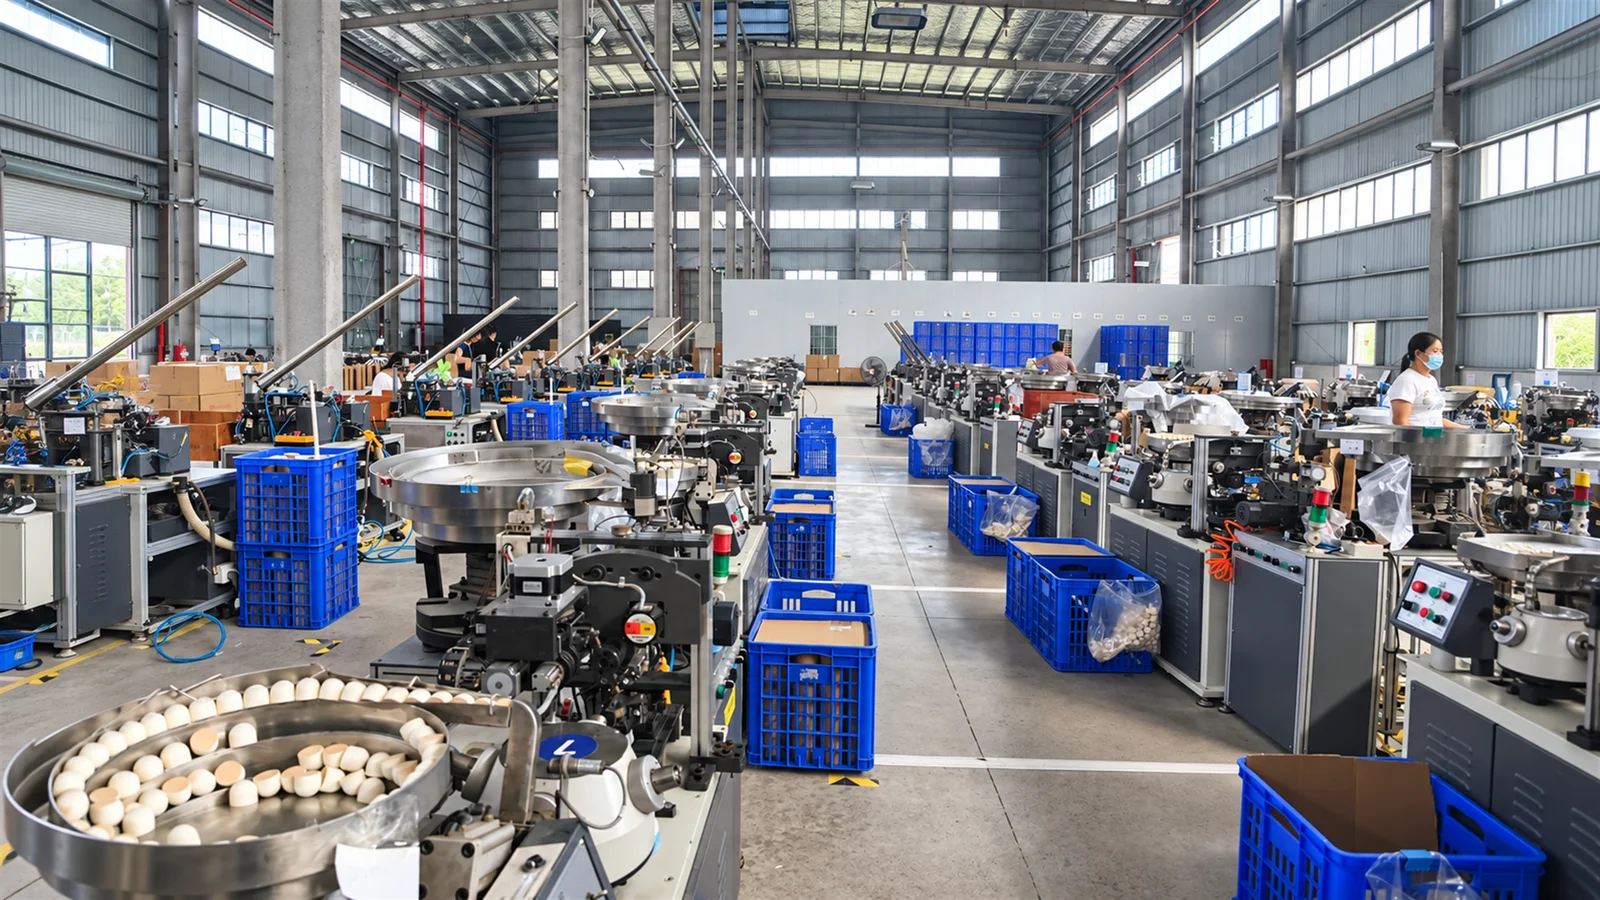
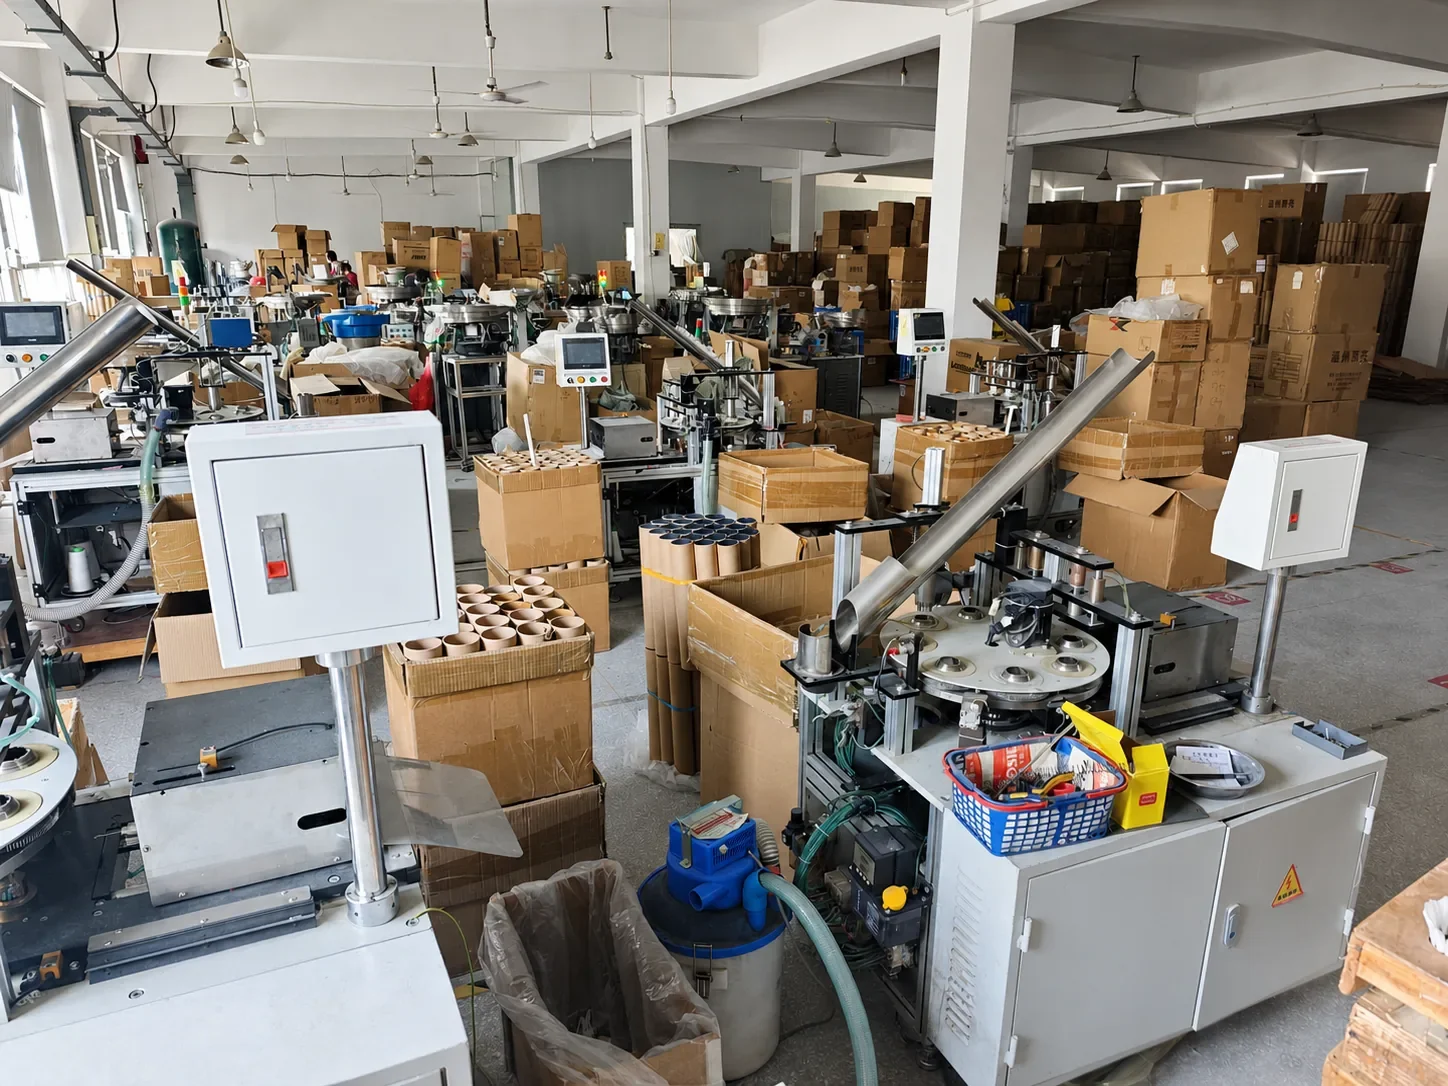
Equipped with automated vibratory bowl feeders for cork bases and synchronized feather guide tracks, ensuring high-precision concentric insertion and seamless automated assembly.

High-rigidity pneumatic guide columns apply uniform downward pressure, embedding feather roots firmly into solid natural cork base sockets without mechanical wobble.

Biaxial coaxial pneumatic grippers clamp the base firmly while optical fiber sensors calibrate vane circumferential spacing to prevent off-center flight bias.

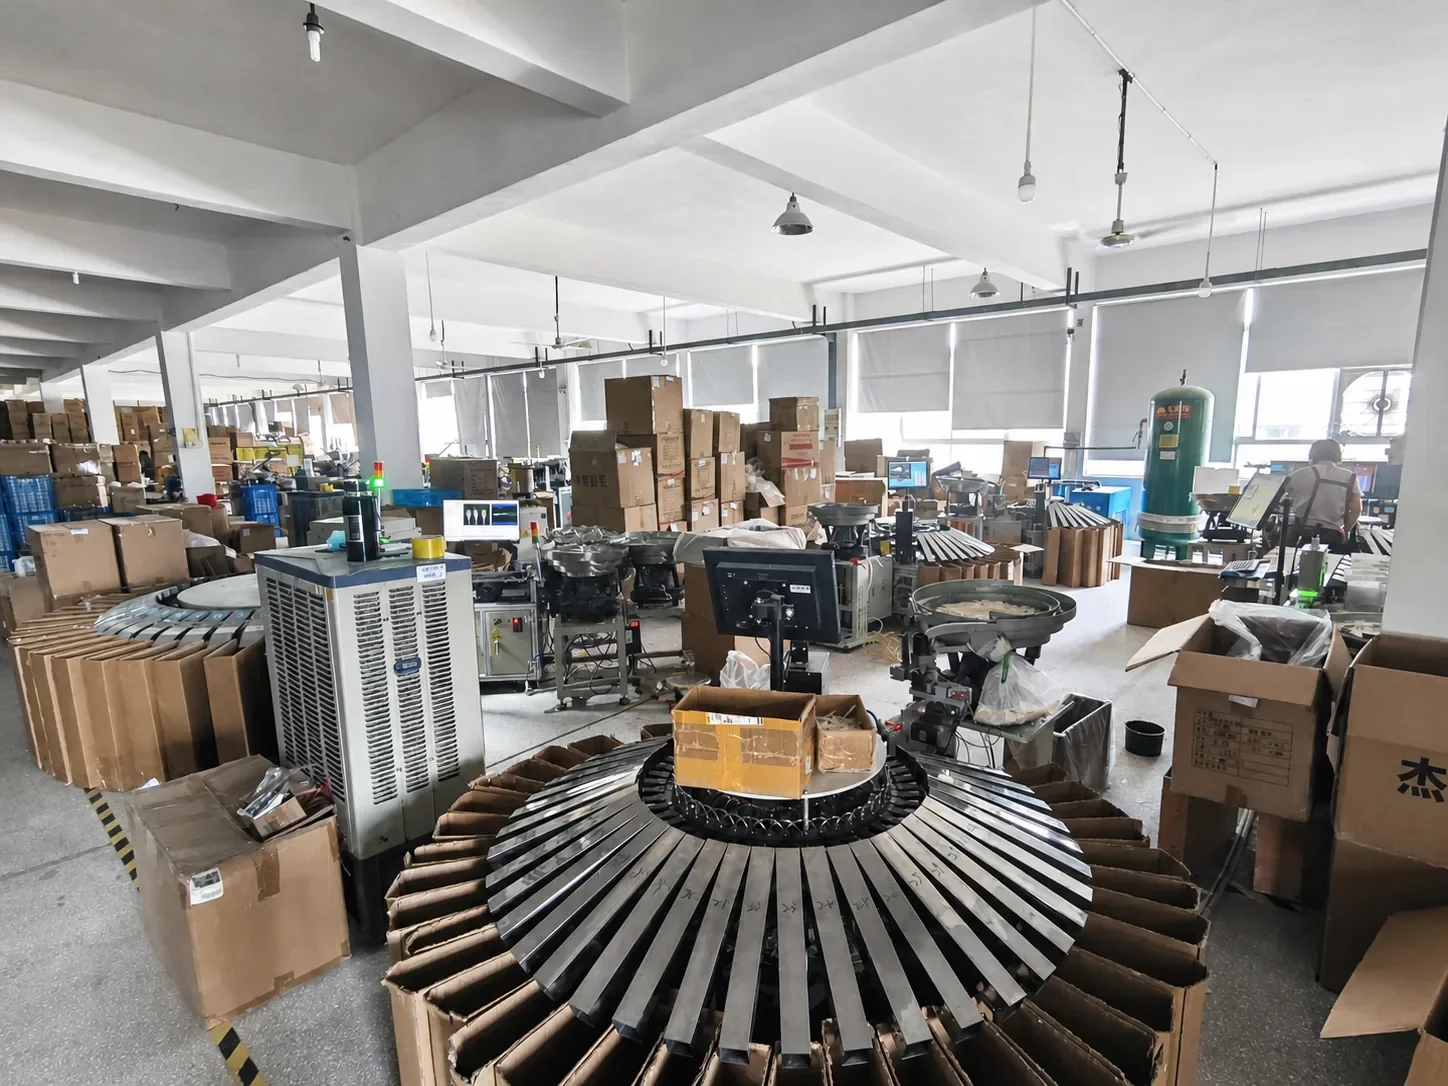
Heavy-duty cam indexing tables step through successive stations for insertion, optical check, and leveling, achieving a first-pass assembly yield over 98.5%.

Dual-axis CNC servo insertion heads plant 16 quills at exact 13.5±0.2mm depths, locking the cone skirt diameter precisely into a 65–68mm concentric circle.

Vertical stabilizing fixtures pair with photoelectric sensors to verify 16-feather tip height alignment and pitch, automatically flagging angular deviations.

Custom perforated matrix staging trays prevent unglued skirts from rubbing or deforming, ensuring smooth transit into subsequent binding and adhesive phases.

Mechanized pushers seat dual natural cotton threads at strict 12mm / 24mm heights, applying calibrated tension knots for maximum impact rebound recovery.

CNC micro-dispensers inject high-elasticity resin into all 16 cork root sockets, maintaining dry adhesive weight strictly at 0.20–0.25g per unit.

Servo motors spin each shuttlecock at high speed as dual adhesive nozzles coat upper and lower thread coils uniformly with polymer resin for superior bond strength.

Units are inverted inside protective sleeves and staged in 30°C / 60% humidity curing rooms for 48 hours, ensuring deep polymer cross-linking without brittleness.

Closed-loop drive systems transport shuttlecocks through heating tunnels with zero mechanical vibration, preventing fluid adhesive shift and center-of-gravity bias.

Senior craftsmen with 10+ years experience trim feather edges with curved stainless scissors and fine-tune vane attack angles with flat pliers, eliminating in-flight wobble.

100% of finished shuttles pass through aerodynamic wind tunnels; high-speed cameras record spin rates (380–450 rpm) and trajectories to grade speed at 75/76/77/78.

Inspected units are categorized by speed and flight grade, resting in pristine conical symmetry before entering moisture-proof aluminum foil tubes.

Finished units are verified within national 4.74–5.50g weight tolerances, automatically tubed (12 pcs/tube), capped, and sealed with tamper-evident security labels.

Packed in heavy-duty 5-ply cartons (50 tubes/carton) on palletized racks, ready for 20ft/40ft container dispatch and global DDP door-to-door delivery.